On this page
How this sealing process works
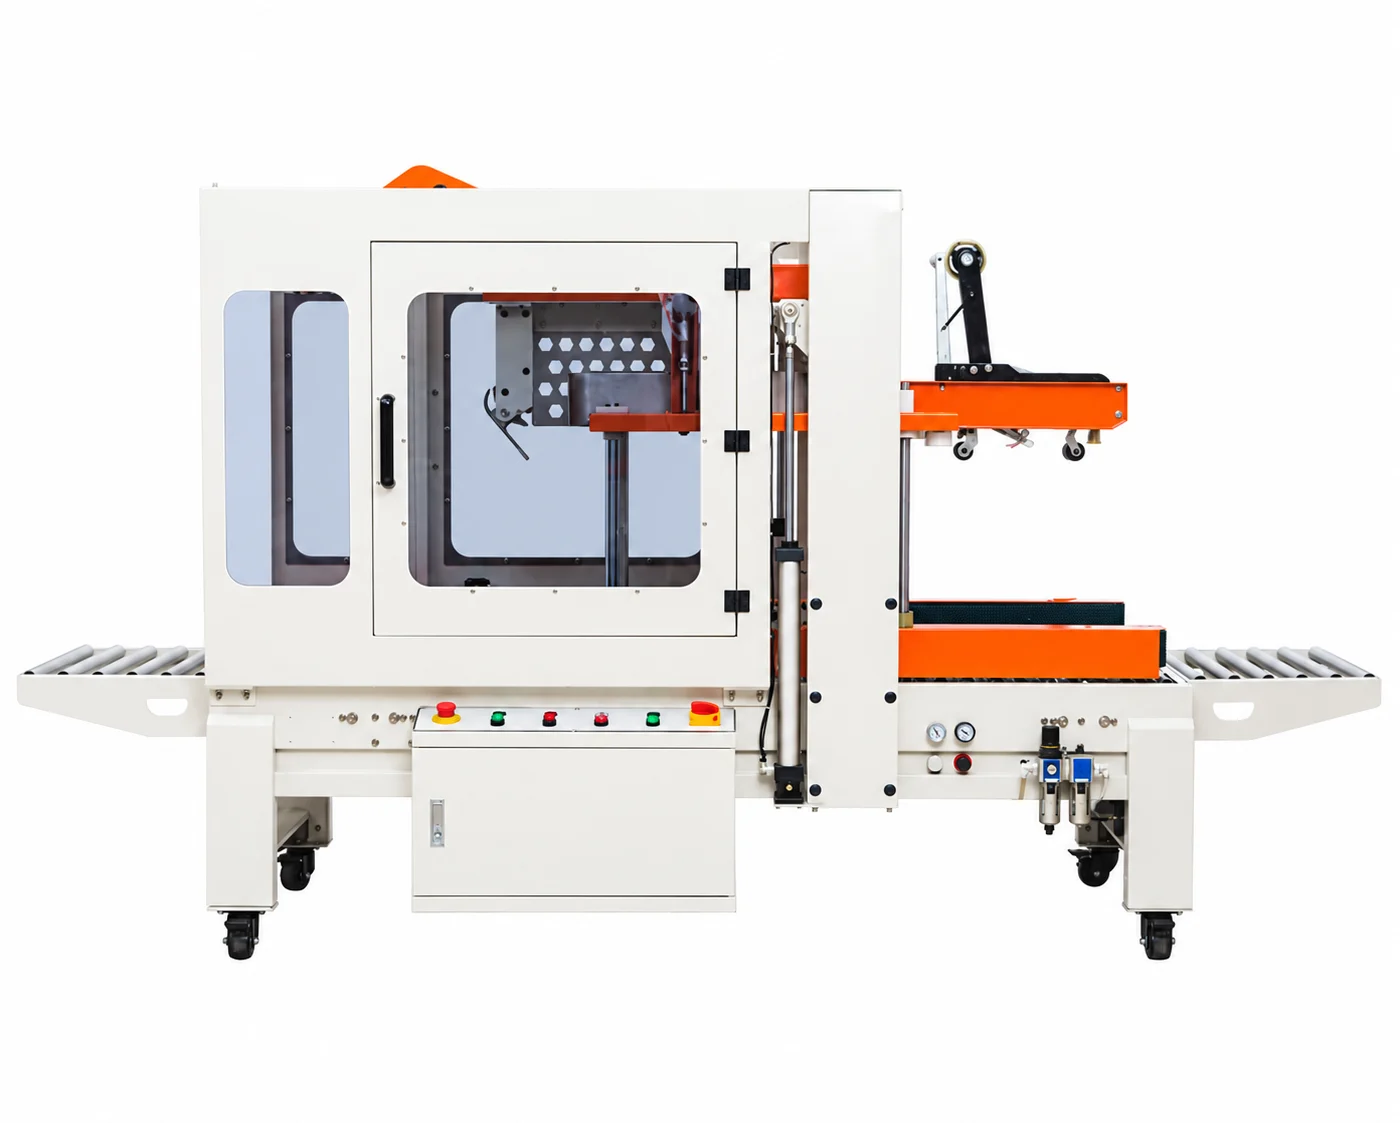
Load carton → Fold upper flaps → Seal centre seams → Discharge
Width and height adjustment
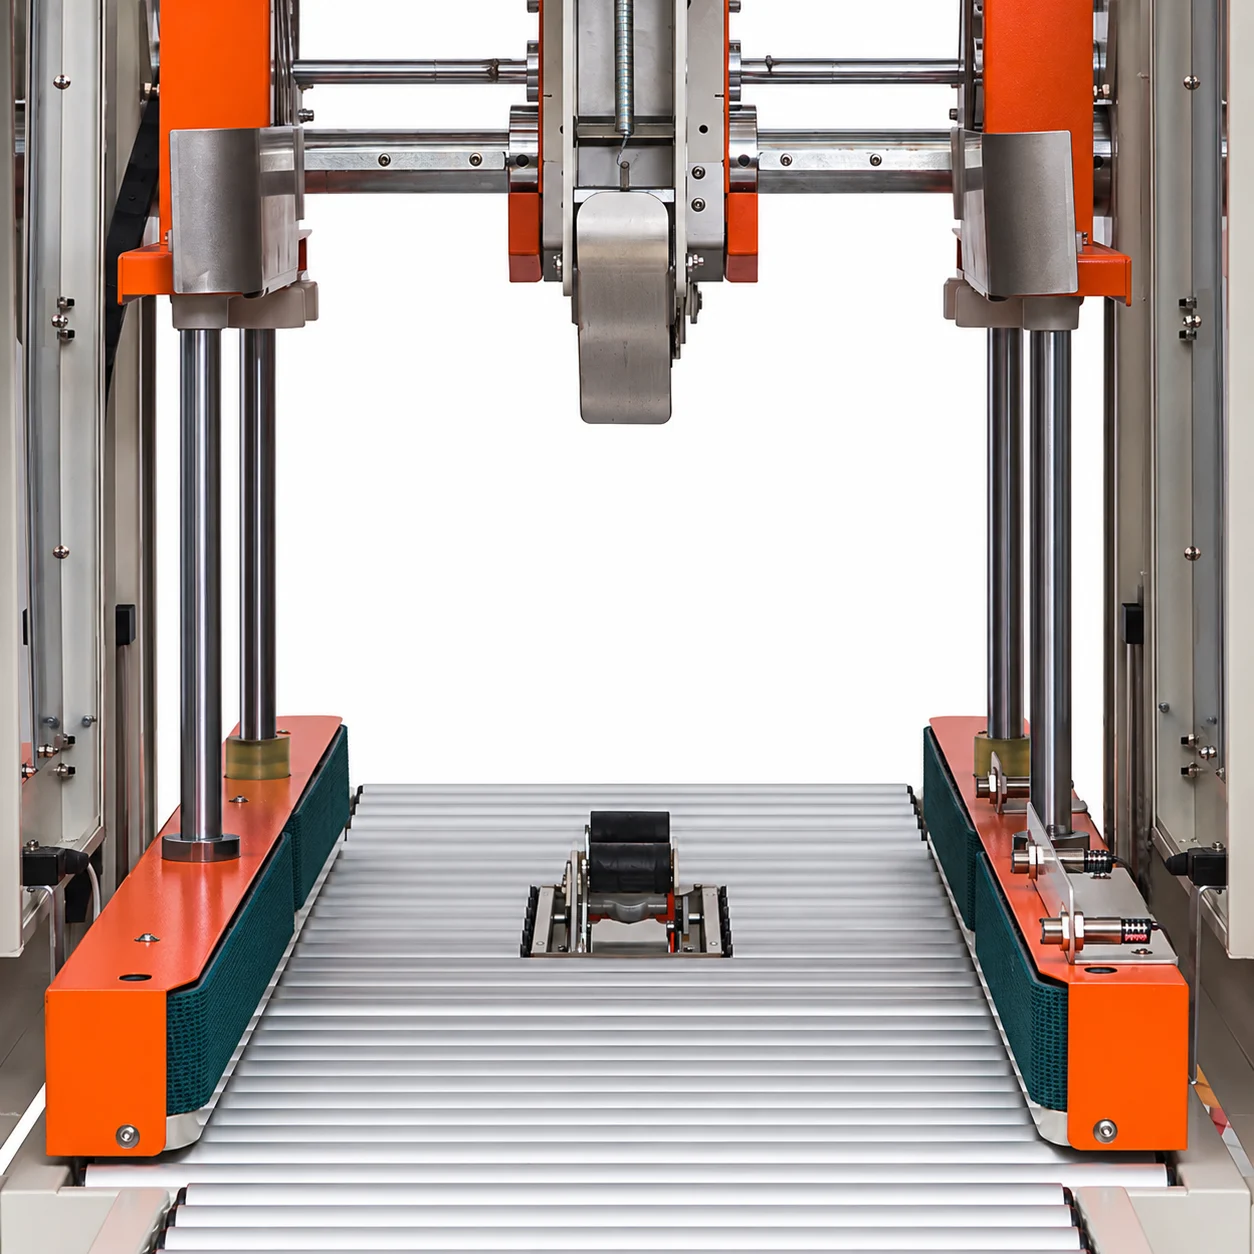
Guided adjustment brings the conveying and sealing assemblies into position for the carton. Define the carton size range and changeover pattern when selecting a setup.
Bottom centre-seam taping
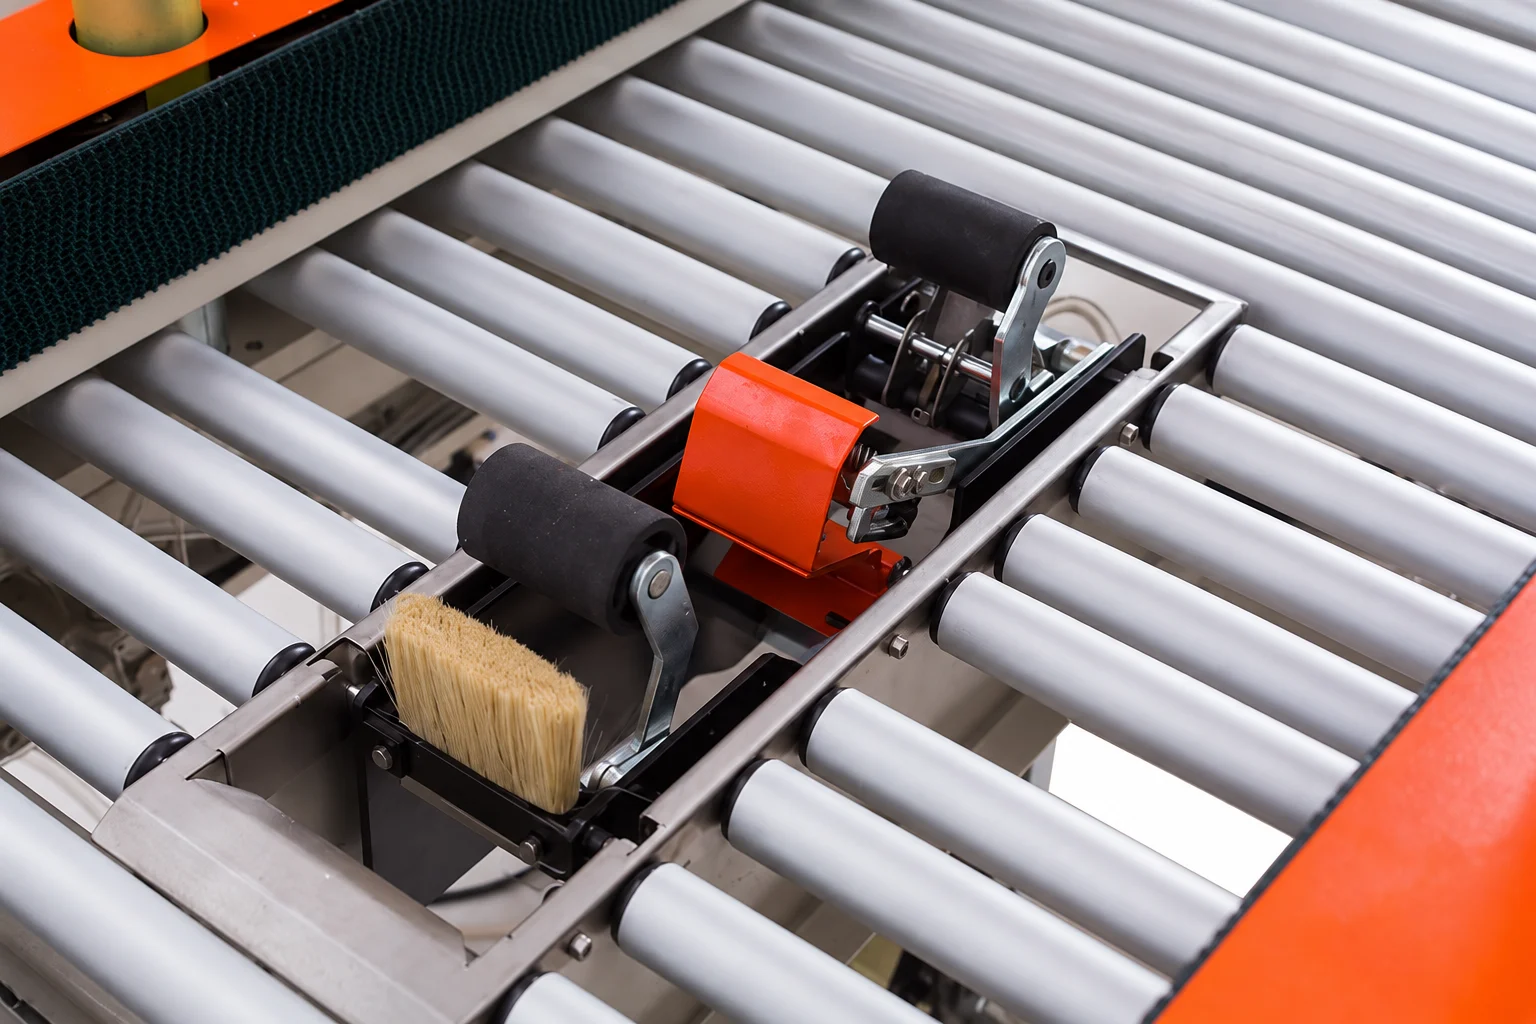
The tape head is integrated into the roller bed. Bottom taping is completed as the carton travels through the machine.
Technical specifications
| Power supply | 220 V / 50 Hz |
|---|---|
| Rated power | 420 W |
| Conveyor speed | 18 m/min |
| Tape width | 48 / 60 mm |
| Carton L × W × H, minimum | 260 × 200 × 160 mm |
| Carton L × W × H, maximum | 700 × 500 × 500 mm |
Conveyor speed does not represent finished cartons per minute. Actual output depends on carton length, spacing and feeding conditions.
Check carton fit before choosing a configuration
Provide carton dimensions, flap style, filled weight, target output and available compressed air. Show how cartons will be fed into the machine.
Compare completed cartons per minute using your actual carton sizes and tape. Conveyor speed alone does not establish finished line output.
Frequently asked questions
Does flap folding also produce an H seal?
Flap folding closes the flaps; this station applies centre-seam tape. An H pattern needs the corresponding edge-sealing stage.
How is the price determined?
An equipment quotation depends on carton sizes, tape requirements, automation scope and included conveyors. Send the application details so that the scope can be defined.